




 Home
 Products

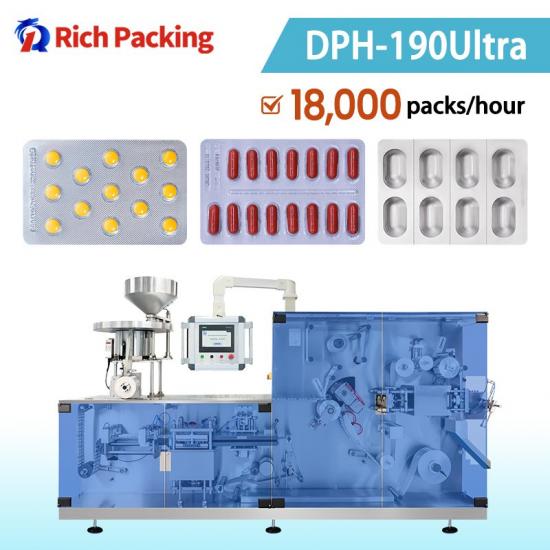
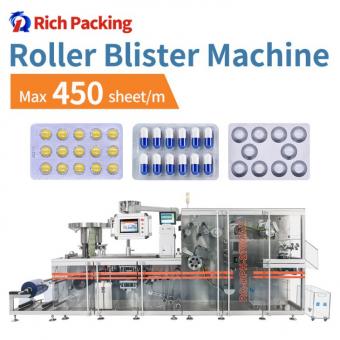
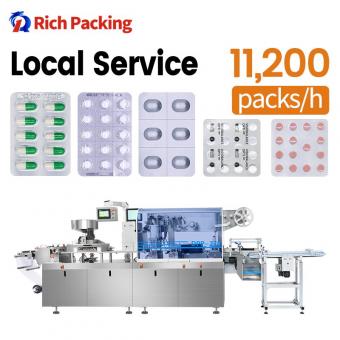
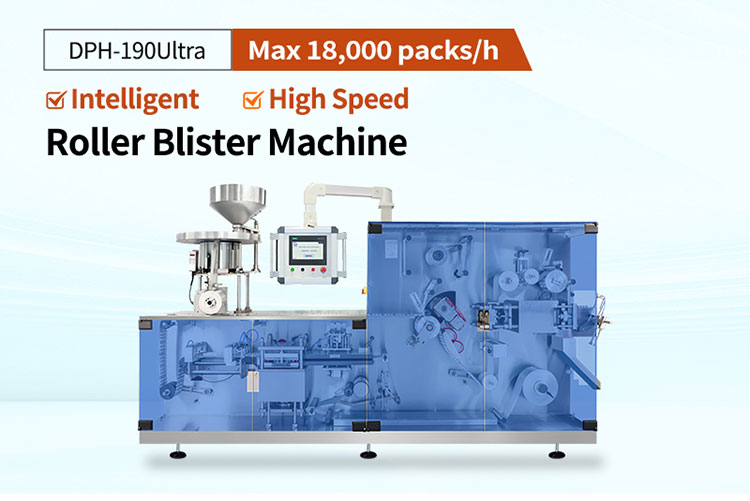
DPH-190Ultra Roller Blister Machine
Want to know about this product?
Feel free to contact me, and I will be more than happy to answer all of your questions.
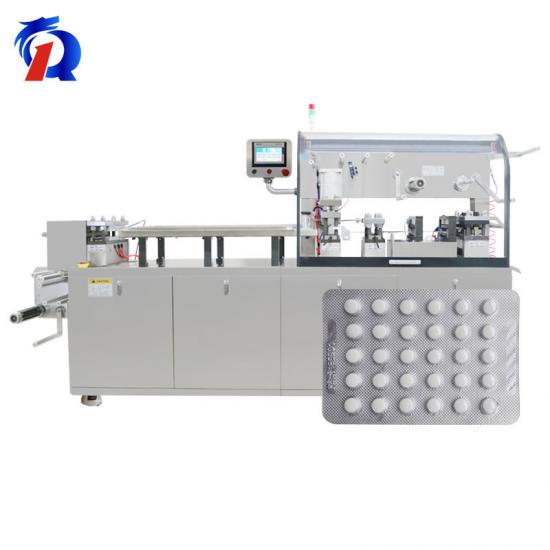
DPH-190Ultra: A Compact Roller-Plate Blister Packing Machine for Pharma and Nutraceuticals
Expanding tablet or capsule production brings a practical packaging question: how can a manufacturer increase blister output while keeping the equipment suitable for its available space and product portfolio? A line that struggles to meet demand can delay shipments, while a larger system may add capacity and installation requirements beyond the project's needs.
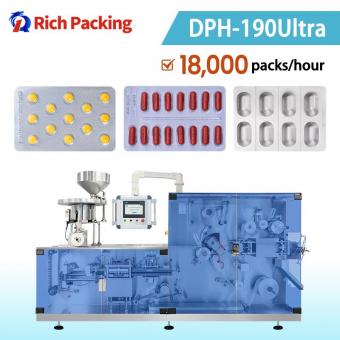
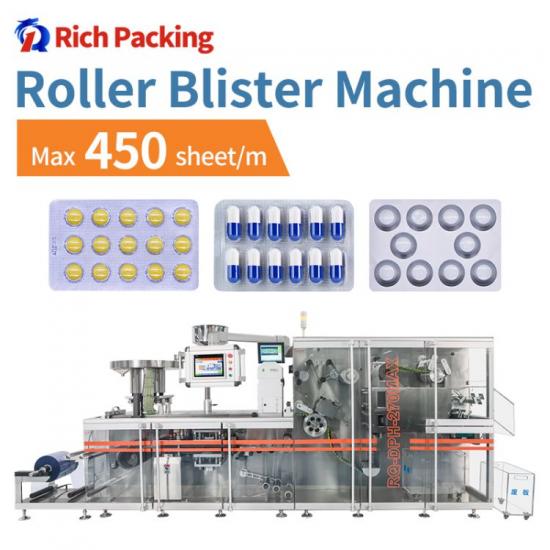
Rich Packing Machinery developed the DPH-190Ultra roller-plate blister packing machine for manufacturers facing this capacity gap. Combining flat-plate forming with roller heat sealing, it offers a rated maximum output of 300 finished blister packs per minute in a three-pack-per-cut layout, equivalent to 18,000 packs per hour.
For pharmaceutical and nutraceutical producers, its value also lies in how the machine handles different products, materials and formats. Servo-controlled forming, traction and cutting, modular tooling and configurable feeding systems help address these requirements within a machine measuring 3,500 x 950 x 1,800 mm.
When Should You Consider a Roller-Plate Blister Packing Machine?
A roller-plate blister packing machine is worth evaluating when packaging has become a constraint on tablet or capsule production. The decision starts with the output required for each product, the duration of production campaigns and the number of formats the line must handle.
An existing flat-plate machine may remain appropriate for a manufacturer's smaller batches or particular packaging requirements. When its achievable output falls below demand, the next step is to assess a system with additional capacity against the same product and blister drawing. Comparing finished packs under equivalent conditions makes that assessment more useful.
The DPH-190Ultra is positioned for pharmaceutical plants, nutraceutical manufacturers and contract manufacturers seeking higher blister output with a compact machine layout. Its modular tooling also makes it relevant where one machine needs to serve several tablet or capsule specifications.
Before selecting a model, review batch sizes, format-change frequency, planned operating hours and downstream capacity. A machine's contribution to production depends on the accepted packs it delivers during the available operating time, including the effects of feeding, rejects and interruptions.
DPH-190Ultra at a Glance: Output, Dimensions and Format Range
The following specifications provide a starting point for evaluating the DPH-190Ultra against a production requirement.
|
Specification |
DPH-190Ultra |
|
Machine structure |
Flat-plate forming with roller heat sealing |
|
Rated maximum output |
Up to 300 finished blister packs/min; 18,000 packs/hour |
|
Maximum-output layout |
Three finished packs per cutting cycle |
|
Cutting frequency |
60-100 cutting cycles/min |
|
Maximum forming area |
230 x 215 mm |
|
Maximum forming depth |
12 mm |
|
Feed stroke range |
160-240 mm |
|
Film width |
170-215 mm |
|
Machine dimensions, L x W x H |
3,500 x 950 x 1,800 mm |
|
Total installed power |
17.5 kW |
|
Machine weight |
2,400 kg |
At 100 cutting cycles per minute with three finished packs per cut, the calculated output is 300 packs per minute. A different blister layout can produce a different number of finished packs at the same cutting frequency. Tablet or capsule throughput also depends on the number of cavities in each pack.
The required operating speed should therefore be established using the actual product, feeder, forming and lidding materials, and approved pack drawing. Define sustained accepted output over an agreed test period, including how rejects and stops will be recorded.
The maximum forming area describes the tooling envelope; finished blister dimensions depend on the selected layout. Installation planning must also include operator access, maintenance clearance, utilities and any connected equipment beyond the machine's listed dimensions.
How Flat-Plate Forming and Roller Sealing Work Together
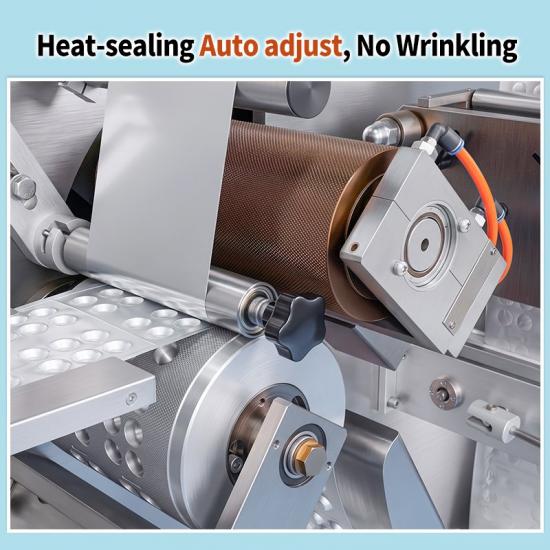
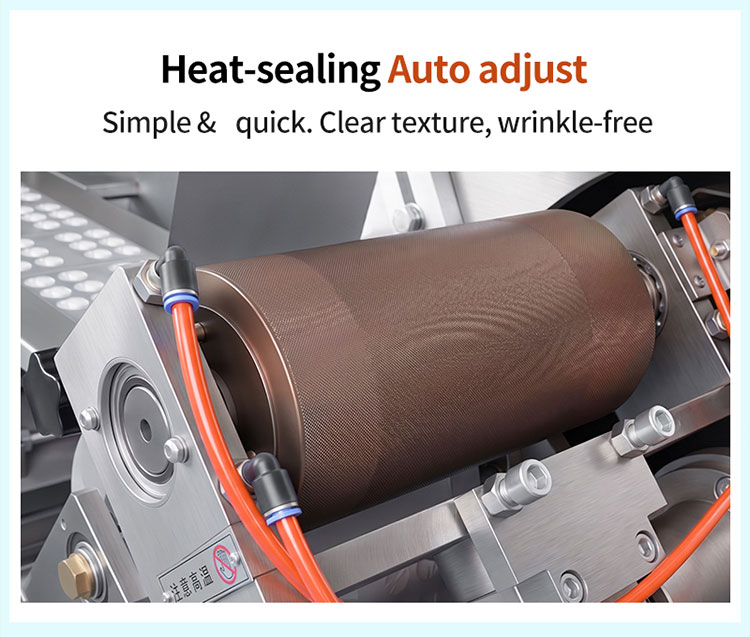
The DPH-190Ultra combines two processes in a roller-plate configuration. Its flat-plate station forms the cavities, while the roller heat-sealing station joins the forming web and lidding material. Controlled movement and material handling help maintain alignment as the web passes through successive operations.
Servo-Controlled Forming, Traction and Cutting
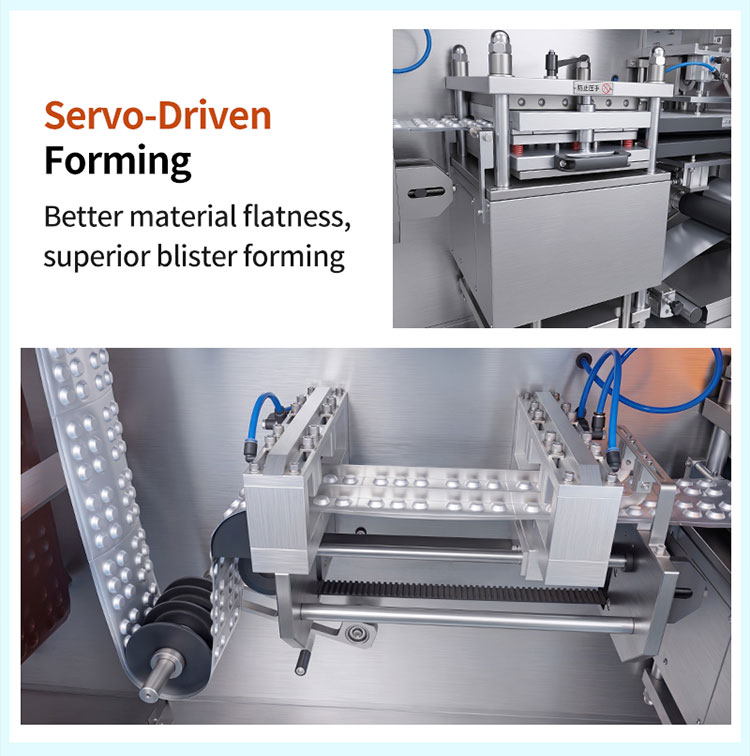
Servo control is applied to forming, traction and cutting. At the forming station, controlled mold movement allows the closing motion to slow as the mold approaches closure. The forming mechanism uses a dual-crank, dual-cam structure with a rated force of 11 tonnes, approximately 110 kN, to support the forming operation.
Servo traction advances the material according to the selected stroke. Operators set the feed length through the HMI and make positional adjustments for the blister format. Servo-controlled cutting feed then supports alignment between the formed web and the cutting tooling.
These functions give operators defined settings for movement and positioning when setting up a format. The one-touch reset function also helps return the servo-controlled mechanisms to their reference positions.
Temperature and Web-Tension Control
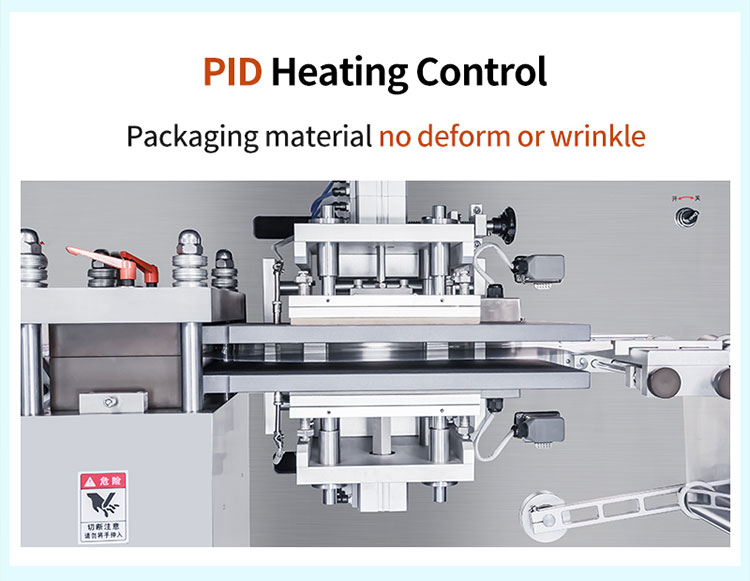
The machine uses segmented PID temperature control at the heating station, with cooling supported by a standard chiller. Heating and cooling settings need to suit the forming material and operating speed.
Foil tension control and web correction address material handling as the reels unwind. A reverse pre-flattening arrangement at the sealing section is designed to help control pack curvature. Together, these features support stable web travel and pack presentation; the sealing settings still need to be established for the selected material construction.
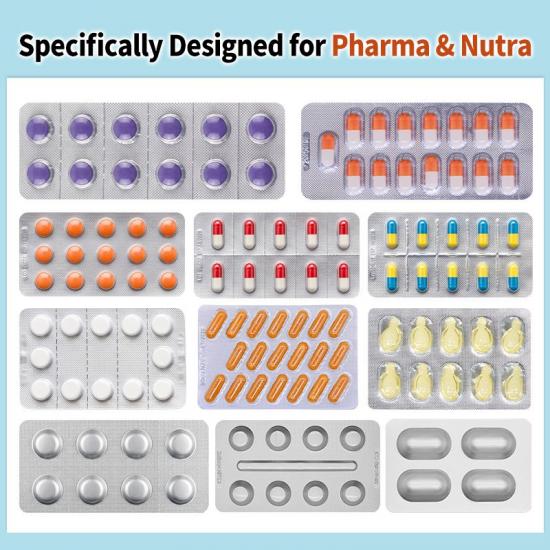
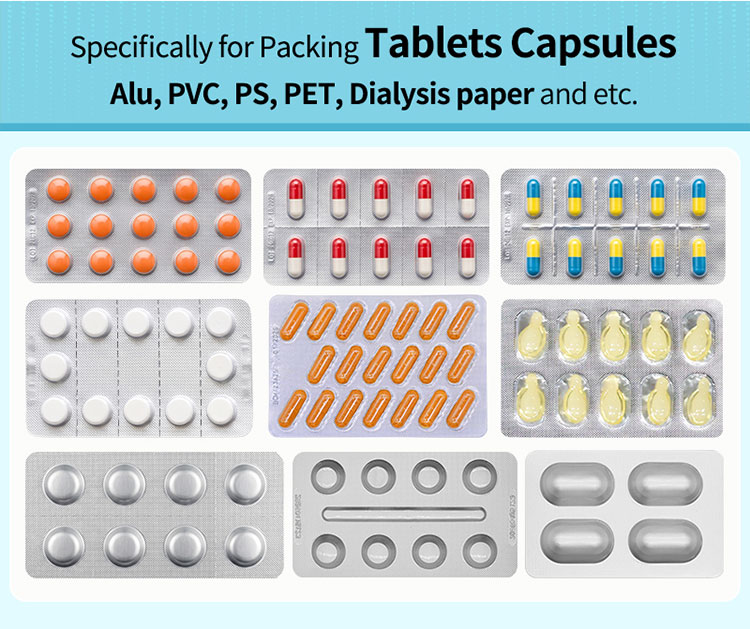
Packaging Tablets and Capsules in Alu-PVC and Alu-Alu Blisters
Product feeding is central to the performance of a pharmaceutical blister packaging machine. Tablet shape, capsule dimensions, surface condition and fragility affect how consistently products enter the cavities. A feeder should be selected around these characteristics and evaluated with representative samples.
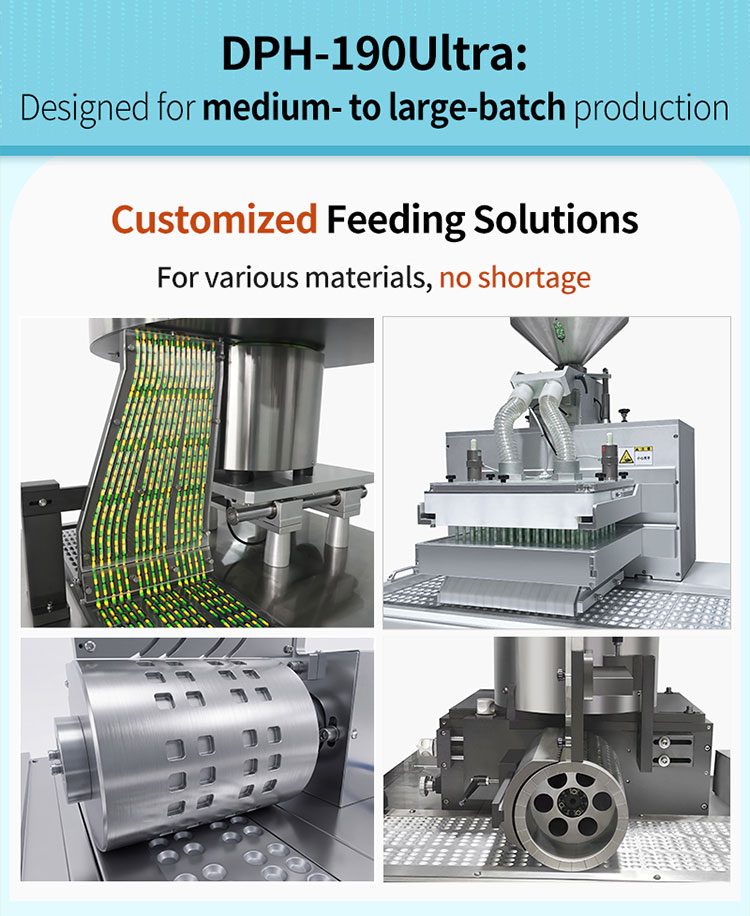
The DPH-190Ultra can be configured with brush, guide-track or roller feeding arrangements. Its adjustable multi-level feeder is intended for tablets and capsules, including suitable shaped tablets. For dusty, uncoated tablets, an optional dust-removal and static-control system can be considered.
For Alu-PVC packaging, the forming and sealing settings must suit the selected plastic film and aluminum lidding foil. Cavity dimensions should accommodate the product while supporting reliable filling and handling.
Alu-Alu packaging requires the corresponding tooling and feeding configuration. The DPH-190Ultra supports conversion through four modular tooling components. A dedicated roller-and-slider feeding arrangement is available for this application to help manage product placement in cold-formed cavities.
Choose the packaging structure using the product's stability data and required barrier performance. Confirm material specifications, tooling and achievable output for each format, including when the same machine will run both Alu-PVC and Alu-Alu packs.
Managing Format Changes and Cleaning Between Batches
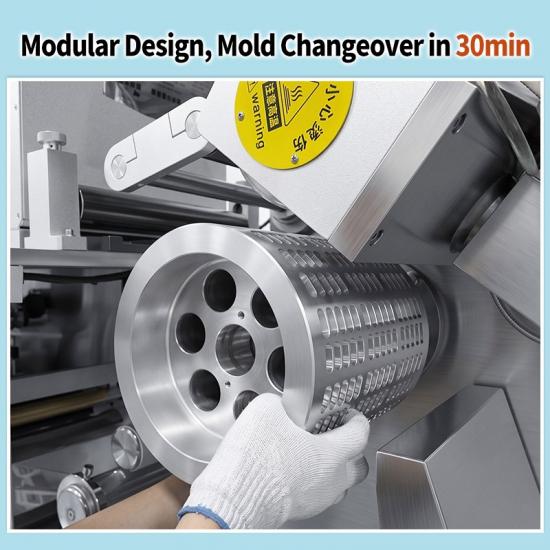
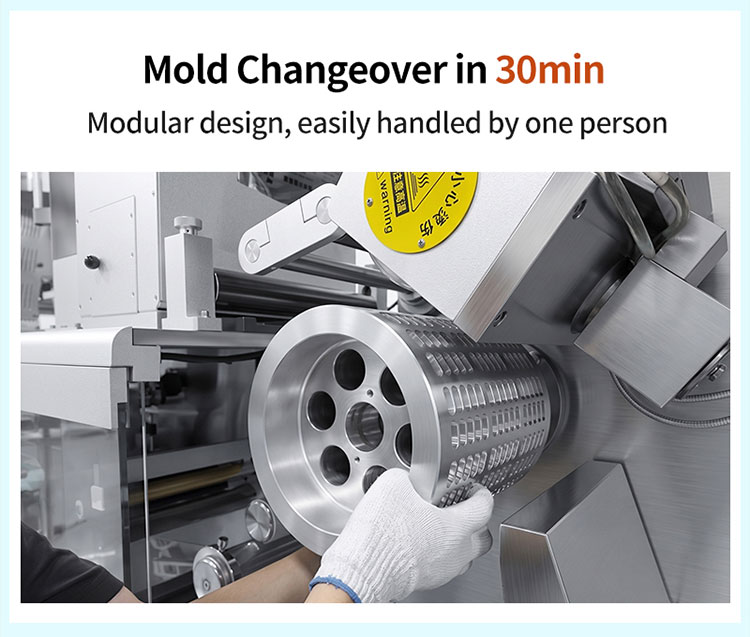
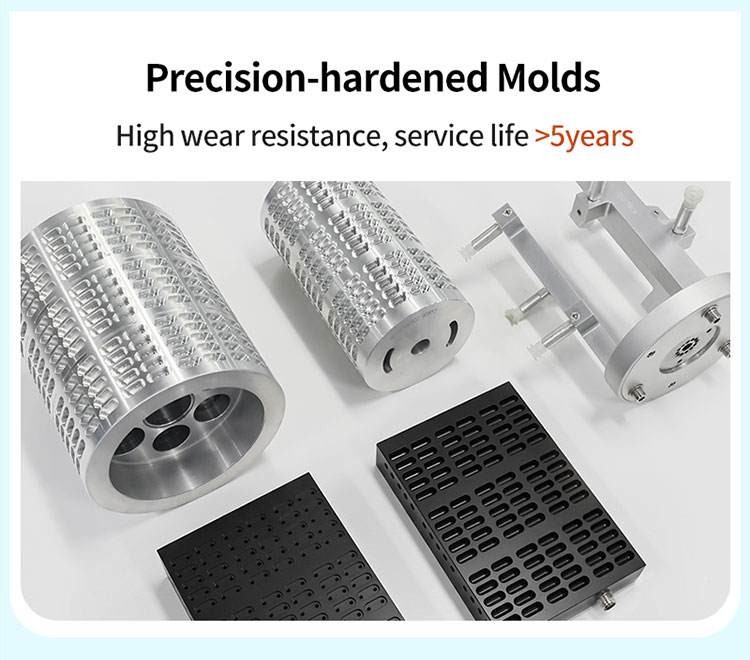
For manufacturers running several products, format changes affect the time available for production. The DPH-190Ultra uses drawer-style tooling and modular stations to simplify mold removal, installation and positioning.
The specified complete mold-set replacement time is within 30 minutes. This provides a useful basis for reviewing the tooling procedure with a trained operator. Cleaning, line clearance, feeder changes and production checks should be timed separately when estimating the complete interval between batches.
The modular layout separates forming, sealing, traction, coding and cutting areas. Mechanical transmission components are located toward the rear of the machine, supporting access for cleaning and maintenance. Cleaning procedures should reflect the products being handled and the manufacturer's own production requirements.
Material use is another part of format planning. The selected cutting layout determines the amount of usable web converted into finished packs and the resulting edge waste. Repeatable positioning can also help reduce unnecessary adjustment runs during setup.
For a meaningful cost comparison, review the proposed blister layout, reel specifications and setup procedure together. Record material use and accepted output during a representative run so that tooling choices can be evaluated against actual production conditions.
Inspection, Data Functions and Cartoning Integration
The DPH-190Ultra can be configured with additional functions to suit the production project. The quotation should identify the selected options and their intended operating scope.
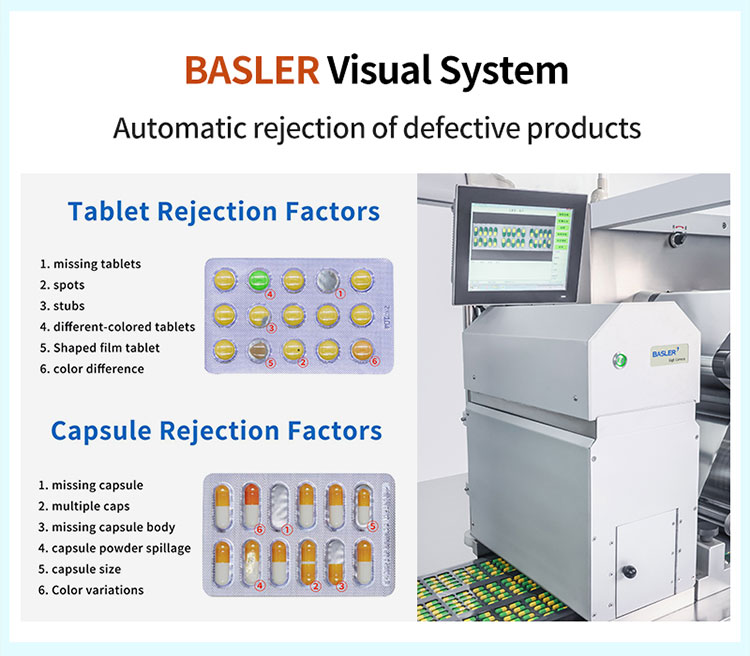
Optional Basler vision inspection and rejection can be considered for missing products, broken tablets, stacked products and specified size or color differences. Detection requirements should describe the defects to be identified, the samples used for testing and the expected rejection behavior. This gives the production and quality teams a clear basis for evaluation.
For digital production projects, discuss MES connectivity and optional OEE or 21 CFR Part 11-related functions. Define the records, user access, interfaces and software verification needed for the installation. This establishes which capabilities belong in the supplied configuration and which depend on the customer's wider systems and procedures.
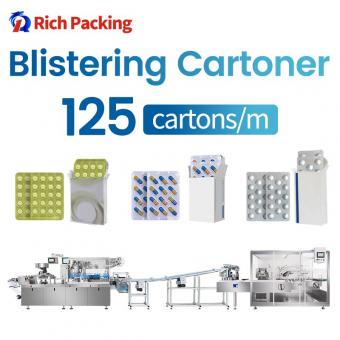
The machine also reserves a program interface for connection to downstream equipment such as a automatic cartoner. Integration planning should cover blister transfer, pack counting, accumulation, control signals and stop/restart behavior.
Cartoning capacity must be calculated using the number of blister packs per carton and the required finished-carton output. Reviewing these interfaces early helps the blister and cartoning sections operate as one coordinated packaging line.
What to Confirm Before Requesting a DPH-190Ultra Quotation
A useful quotation begins with a clear description of the packaging task. Send Rich Packing Machinery the following information:
· Product samples, dimensions, shape and relevant handling characteristics.
· A dimensioned blister drawing, including cavities per pack and coding requirements.
· Forming and lidding material specifications, thicknesses and reel dimensions.
· Target sustained accepted output, batch sizes and expected format-change frequency.
· Required inspection, rejection, software and downstream integration functions.
· Available space, site utilities, technical-document requirements and installation needs.
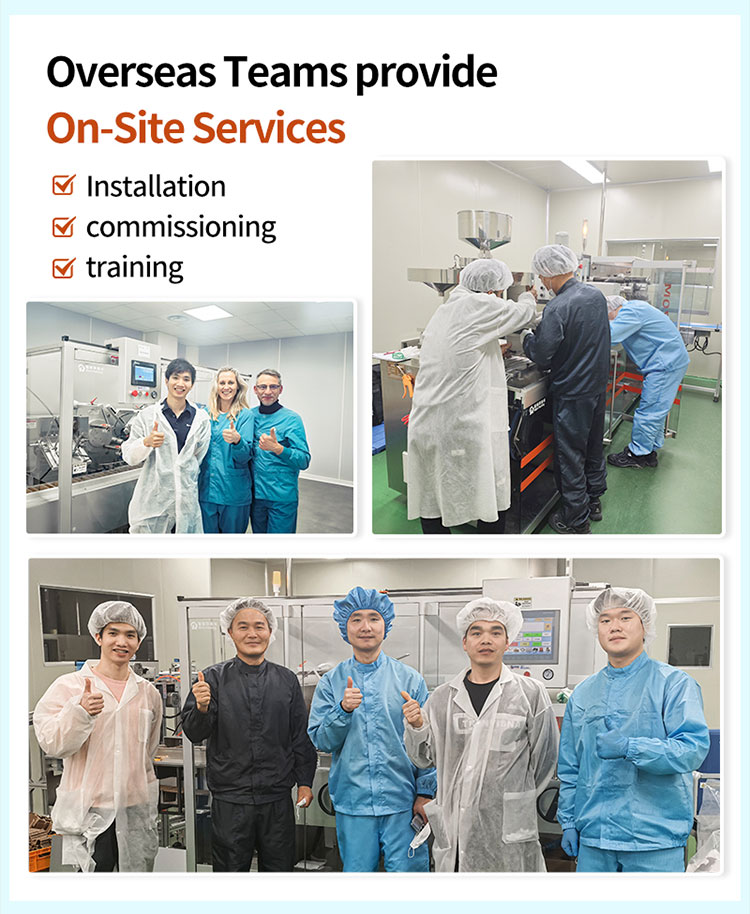
For facilities in North America, Europe, the Middle East and Southeast Asia, overseas project planning should address the actual site conditions. Confirm electrical voltage and frequency, compressed air, cooling, access routes, operating language and the required training and service arrangements. The DPH-190Ultra's electrical supply can be customized within the documented 110-410 V, 50/60 Hz range; the exact supply must be specified for the ordered machine.
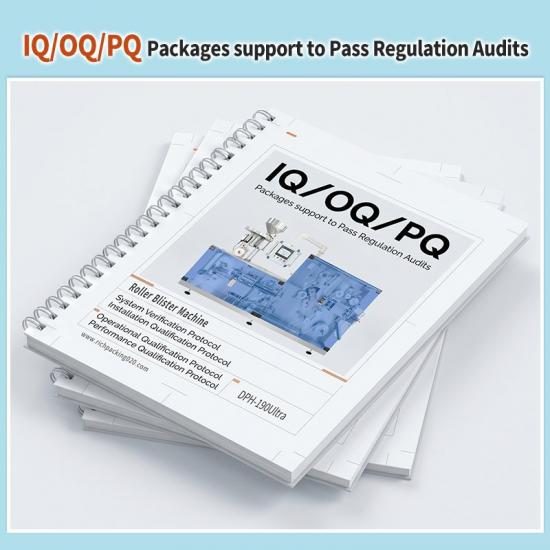
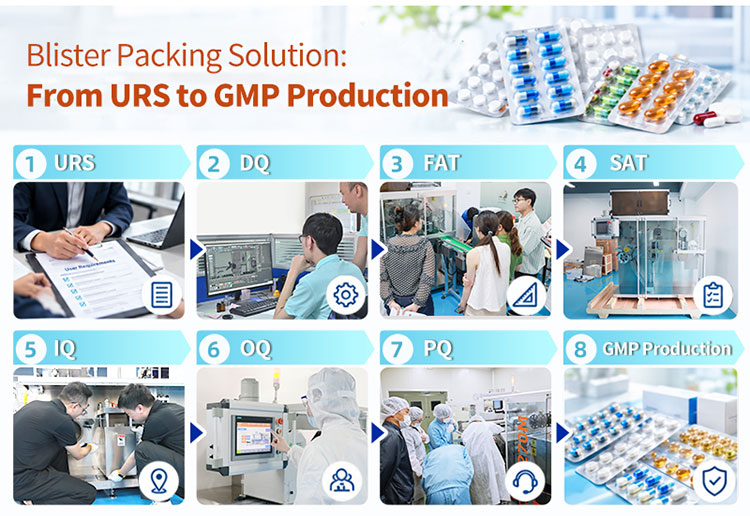
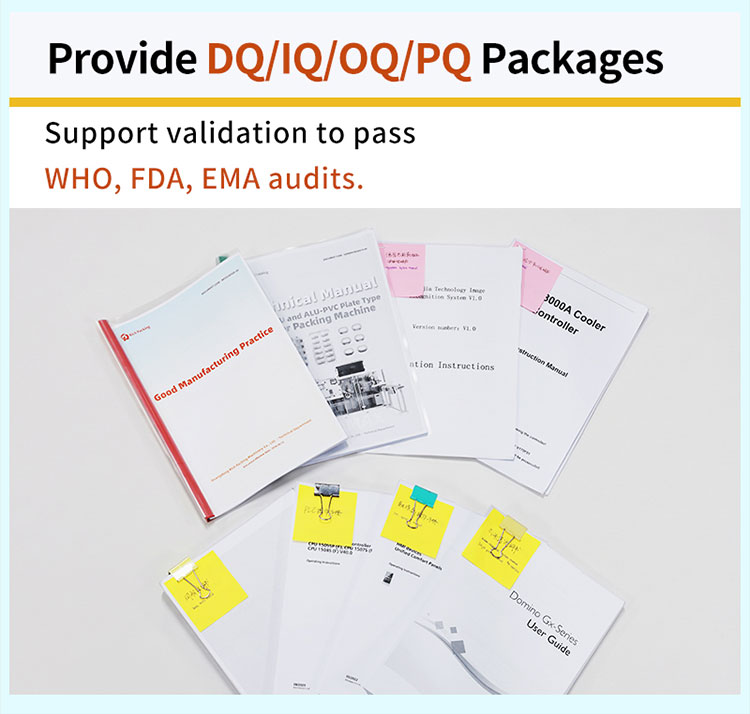
Agree a factory acceptance test, or FAT, around the proposed products, materials and formats. Useful acceptance points include sustained output, forming and sealing results, feeding behavior, inspection challenges, format changes and relevant line interfaces. Specify the required technical documents and qualification-support scope in the purchase agreement.
Request a DPH-190Ultra Configuration Review
Share your tablet or capsule samples, target blister format and production requirements with Rich Packing Machinery to discuss the appropriate feeder, tooling, options and line layout.
FAQ: DPH-190Ultra Blister Packing Machine
1. What type of blister packing machine is the DPH-190Ultra?
It is a roller-plate blister packing machine combining flat-plate forming with roller heat sealing. Forming, traction and cutting use servo control.
2. What is its maximum production output?
The rated maximum is 300 finished blister packs per minute, or 18,000 per hour, with three packs per cutting cycle. Actual output depends on the product, materials and layout.
3. Can it package pharmaceutical and nutraceutical tablets and capsules?
Yes. Feeders and tooling are selected for the product's dimensions, shape and handling characteristics. Representative samples should be evaluated before configuration approval.
4. Does it support both Alu-PVC and Alu-Alu packaging?
Yes, with the corresponding tooling and feeding configuration. Material specifications and achievable output should be confirmed separately for each application.
5. How long does a mold change take?
The specified complete mold-set replacement time is within 30 minutes. Cleaning, line clearance and production checks require separate time allowances.
6. How much installation space is required?
The listed machine dimensions are 3,500 x 950 x 1,800 mm. Allow additional space for operator access, maintenance, utilities and connected equipment.
7. Is vision inspection included?
Basler vision inspection and rejection are optional. Specify the required defect checks and verify performance with representative products and defect samples.
8. Are 21 CFR Part 11-related functions available?
Related software functions are optional. Define the required records, controls, interfaces and verification scope when specifying the project.
9. Can the DPH-190Ultra connect to a cartoning machine?
A program interface is reserved for downstream connection. Blister transfer, pack counting, operating speeds and control signals require project-specific integration review.
10. Can the electrical supply suit an overseas installation?
The documented customizable range is 110-410 V at 50/60 Hz. Confirm the exact site supply and final electrical configuration before ordering.
11. What should buyers confirm about FAT and technical documents?
Agree the test products, materials, run conditions and acceptance criteria. List the required manuals, drawings and qualification-support documents in the purchase agreement.
12. How are price and delivery time determined?
They depend on tooling, feeders, inspection, software options and integration scope. Submit samples, a blister drawing and output requirements for a project-specific quotation and schedule.
 IPv6 network supported